Explore our flagship OEM micro-generator systems and structural tower platforms designed for rooftop, off-grid, agricultural, and industrial hybrid installations worldwide.
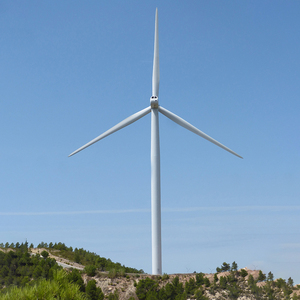

An authoritative engineering synthesis on structural monopole integrity, direct-drive turbine tower dynamic load management, and turnkey procurement optimization for distributed energy resources (DER).
Modern wind turbine tower design demands rigorous Finite Element Analysis (FEA) to withstand complex aerodynamic loads. OEM towers must absorb combined bending moments, axial thrust, and torsional shear generated by rotor rotation and transient turbulence gusts exceeding 60 m/s (IEC 61400-2 Class I compliance).
By executing dynamic resonance calculations, engineered tapered monopoles avoid resonant frequencies matching the turbine's 1P (rotor speed) and 3P (blade passing rate) excitation bands, eliminating long-term structural fatigue.
Structural integrity hinges on high-tensile hot-rolled steel plates such as Q355B, Q355D, S355JR, and S355J2+N. OEM tower steel sections undergo automated submerged arc welding (SAW) to achieve 100% full-penetration longitudinal and circumferential joints.
Every welded seam undergoes mandatory Non-Destructive Testing (NDT), including Ultrasonic Testing (UT) and Magnetic Particle Inspection (MPI) to guarantee zero microscopic voids under extreme cold-climate impact toughness testing down to -40°C.
Offshore, coastal, and high-salinity agricultural sites demand heavy-duty corrosion defense. OEM export towers utilize a multi-stage surface preparation conforming to ISO 8501-1 Sa 2.5 blast cleaning prior to hot-dip galvanizing (minimum 85 µm zinc layer thickness) or thermal spray aluminum coating.
For harsh marine environments, a multi-layer epoxy resin finish with polyurethane topcoat engineered under ISO 12944 C5-M specification provides an operational lifespan exceeding 30 years without major paint maintenance.
Selecting the appropriate structural configuration based on hub height, soil foundation mechanics, logistics footprint, and turbine drivetrain capacity.
| Tower Type Architecture | Target Turbine Capacity | Height Range (m) | Corrosion Protection | Foundation Requirement | Key Advantage & Best Application |
|---|---|---|---|---|---|
| Tapered Tubular Steel Monopole | 1 kW - 90 kW (S-Series / M-Series) | 12m - 36m | Hot-Dip Galvanized / C5-M Epoxy | Gravity Base / Micropile Anchor | Minimal land footprint, clean aesthetics, enclosed internal ladder & wiring conduit. Ideal for commercial & agricultural sites. |
| Hydraulic Tilt-Over Monopole | 300W - 10 kW Micro-Turbines | 9m - 18m | Hot-Dip Galvanizing (85 µm+) | Reinforced Concrete Pad | Enables ground-level maintenance without cranes. Perfect for remote microgrids, telecom towers, and extreme weather zones. |
| Modular Lattice Structural Tower | 5 kW - 250 kW Systems | 18m - 50m | HDG Zinc Immersion | Multi-Leg Concrete Footings | Lowest material weight ratio, modular containerized ocean freight. Superior performance for mountainous and remote off-grid locations. |
| Guyed Steel Tubular Shaft | 80mW - 3 kW Small Wind | 6m - 15m | Powder Coating / Electro-Galv | Ground Anchor Pins & Center Pad | Ultra-low cost procurement, rapid field installation. Best suited for temporary monitoring, street lighting, and domestic power. |
The global wind energy supply chain is transitioning toward decentralized generation, hybrid energy storage integration, and intelligent predictive maintenance capabilities.
Traditional gearboxes represent the single most common failure point in small-to-medium scale wind turbines due to continuous mechanical shear and lubrication degradation. Global procurement managers are rapidly transitioning toward direct-drive Permanent Magnet Generator (PMG) systems, such as our EOX M-26 (90 kW) platform.
OEM wind towers are now custom-engineered with wider top flange diameters and internal structural stiffeners specifically calculated to support the increased mass of high-torque direct-drive low-RPM generators, completely eliminating gearbox oil changes and reducing scheduled annual maintenance to simple visual inspections.
Commercial and industrial energy consumers no longer procure standalone power generation assets. Future-ready OEM towers are designed with integrated structural brackets and base cabinet housings to form EOX WS²+ integrated wind-solar-storage systems under a single master AI-driven Energy Management System (EMS).
By utilizing the bottom 3 meters of the steel monopole as an climate-controlled housing box for battery energy storage systems (BESS) and inverter modules, site operators achieve maximum clean energy density per square meter of land without requiring additional real estate or building permits.
Next-generation OEM exporters are embedding continuous IoT strain gauges, tri-axial MEMS accelerometers, and acoustic emission sensors directly inside the tower shaft during fabrication. Real-time telemetry streams into centralized SCADA platforms to detect bolt pre-load decay, tower tilt, and foundation micro-settlement.
Predictive analytics algorithms notify asset managers prior to fatigue thresholds being breached, guaranteeing fleet availability above 98% throughout a 30-year operational lifecycle in remote agricultural feedyards and harsh sub-zero microgrids.
Global freight prices have elevated transportability into a primary purchasing criterion. Advanced OEM wind towers are manufactured in modular flanged sections precisely dimensioned to fit inside standard 40ft High-Cube (40HC) shipping containers without requiring breakbulk heavy lift vessels.
Standardized precision-machined connection flanges with high-strength Grade 10.9 hot-dip galvanized bolt sets enable local construction crews to erect 30m-36m monopoles within 48 hours, significantly slashing crane rental overhead and civil mobilization costs.
Combining North American and global engineering rigor with state-of-the-art automated manufacturing infrastructure to deliver robust, predictable distributed clean energy.
Founded in Montréal, Canada in 2001, our engineering team pioneered direct-drive permanent magnet wind architecture. Our structural designs have been field-tested in demanding environments worldwide—from Alberta winter freezes and Scottish coastal gales to Belgian maritime air and dust-laden Colorado feedyards.
We provide complete end-to-end manufacturing flexibility: custom top-flange drilling patterns tailored to your proprietary nacelle, variable hub height sections from 6m to 48m, specialized base door cutouts for internal control cabinets, and custom color options complying with local aviation/zoning codes.
Every OEM tower section is manufactured in ISO 9001, ISO 14001, and ISO 4501 certified facilities. We provide comprehensive documentation packages with every export shipment, including Mill Test Reports (MTR), NDT inspection certificates, 3D laser flange flatness reports, and galvanizing thickness verifications.
Comprehensive technical and commercial responses to common buyer inquiries regarding tower selection, wind resource thresholds, OEM manufacturing lead times, and shipping logistics.
Contact our structural engineering and global export team today. Provide us with your turbine specifications or project coordinates for a comprehensive site assessment, structural drawing proposal, and direct factory quote.